The Distinction From General Elevator Manufacturers
Most elevator manufacturers produce products for offices, hotels, retail centers, and residential buildings. A hospital elevator manufacturer operates in a different segment of the market. The products are engineered for the specific demands of healthcare, and the differences go far beyond size.
A standard commercial elevator might have a capacity of 1,000 to 1,600 kilograms and a car size suitable for passengers and light loads. A hospital bed elevator typically has a capacity of 2,500 kilograms or more, with a car large enough to accommodate a hospital bed, medical equipment, and the staff required to manage the patient during transport. The door opening is wider, often 1,400 millimeters or more, to allow beds and equipment to pass without obstruction.
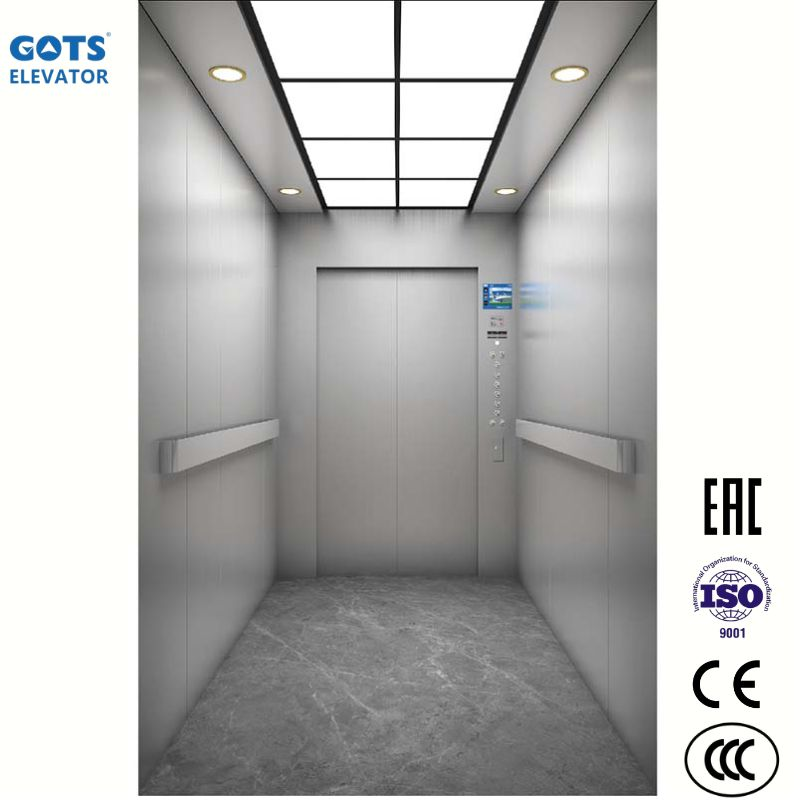
The interior finishes are different. Hospital elevators use stainless steel and other non-porous materials that can withstand aggressive cleaning and disinfection. The surfaces are smooth and seamless, with no crevices where bacteria can accumulate. The lighting is bright and even, supporting clinical observation. The ventilation is robust, ensuring air quality in an enclosed space where patients may be vulnerable.
The Product Categories
Hospital elevator manufacturer typically produce several categories of elevators, each designed for a specific function within the healthcare environment.
Bed elevators are the most specialized. They are designed specifically for transporting patients on beds and stretchers. The car dimensions are standardized to accommodate a standard hospital bed with the head or foot raised, along with IV poles, monitors, and other equipment. The doors are wide and open fully, allowing the bed to be rolled in and out without maneuvering. The ride quality is smooth, with precise leveling to prevent jolts that could disturb the patient or dislodge equipment.
Stretcher elevators are a related category, slightly smaller than bed elevators but designed for stretchers and wheelchairs. They are often used in outpatient areas, emergency departments, and diagnostic imaging suites.
Service elevators are designed for staff, supplies, and waste. They are separate from patient elevators to maintain infection control and traffic separation. Clean supplies move on one path, soiled materials on another. Service elevators may be larger and more robust than passenger elevators, capable of handling carts, pallets, and heavy equipment.
Visitor and staff elevators handle the general traffic of the hospital. They are designed for comfort, efficiency, and durability, with finishes that are easy to clean and maintain.
Freight elevators handle the heaviest loads, including food service carts, laundry, and equipment deliveries. They may be located near loading docks and service corridors, separate from patient and visitor areas.
The Safety and Reliability Requirements
Hospital elevator manufacturers must meet safety standards that exceed those for commercial elevators. The consequences of failure are more severe. A stalled elevator carrying a patient to surgery is not an inconvenience. It is a medical emergency.
The emergency operation features are more comprehensive. Hospital elevators must be equipped with automatic rescue devices that bring the car to the nearest landing in the event of a power failure. Battery backup systems must be capable of operating the elevator for a specified period, allowing critical transport to continue. Emergency communication systems must connect directly to a monitored station, not just an automated answering service.
The fire service features are also more demanding. Hospital elevators must be able to operate under fire service conditions, allowing firefighters to use them for evacuation and rescue. The controls must be designed for use by emergency personnel, with clear labeling and simple operation.
The reliability standards are higher. Hospital elevators are expected to operate continuously with minimal downtime. Maintenance programs must be proactive, with regular inspections and preventive replacement of components before they fail. Many manufacturers offer remote monitoring systems that track performance and alert service technicians to potential problems before they become failures.
The Hygiene and Infection Control Requirements
Infection control is a primary concern in healthcare facilities, and hospital elevator manufacturers must design their products to support it.
The interior surfaces must be non-porous, seamless, and resistant to the chemicals used in hospital cleaning. Stainless steel is the most common material, but some manufacturers use other materials that offer similar performance.
The elevator must be easy to clean thoroughly. There should be no crevices, no fabric, and no surfaces that cannot be reached with cleaning equipment. Some manufacturers offer designs with removable panels or access points that allow for deep cleaning.
The ventilation system must be capable of filtering and exchanging air to reduce the concentration of airborne pathogens. Some hospitals require negative pressure or positive pressure conditions in specific elevators, depending on the patients they transport.
The controls must be touchless or easily disinfected. Touchless controls using infrared sensors or proximity detection are increasingly common. Where physical buttons are used, they must be designed for easy cleaning and resistance to disinfectants.
What to Consider When Selecting a Manufacturer
The selection of a hospital elevator manufacturer is a long-term decision. The elevators will be in service for decades, and the manufacturer will be responsible for supporting them throughout their life.
The manufacturer’s experience in healthcare is the first consideration. A manufacturer who has installed elevators in hospitals understands the unique requirements of the environment. A manufacturer who has only served commercial buildings may not.
The manufacturer’s product range is the second consideration. The hospital may need bed elevators, service elevators, visitor elevators, and freight elevators. A manufacturer who can supply all of these from a single source simplifies procurement, installation, and maintenance.
The manufacturer’s service and support capabilities are the third consideration. Elevator maintenance in a hospital is not a routine task. It requires technicians who understand the equipment, access to spare parts, and a response time that minimizes downtime. The manufacturer’s service network and parts availability must be adequate for the facility’s location and requirements.
The manufacturer’s references are the fourth consideration. Hospitals that have installed the manufacturer’s elevators can provide feedback on performance, reliability, and service. This information is more valuable than any specification sheet.
The Bottom Line
A hospital elevator manufacturer builds vertical transportation systems for an environment where failure is not an option. The products are engineered for size, durability, hygiene, and reliability that exceed commercial standards. The manufacturers who serve this market have developed specialized expertise that general elevator manufacturers do not possess. For healthcare facility planners and procurement professionals, understanding what these manufacturers do and how to evaluate them is essential to ensuring that patients, staff, and supplies move safely and efficiently throughout the facility.